Leave Your Message

How to Choose Gyratory Crusher Wear Parts?

Choosing Gyratory Crusher Wear Parts is not a simple matter of matching a part number. These components work under heavy, repeated impact and compression, while ore characteristics change from one site to another. The scale is substantial: the U.S. Geological Survey’s Mineral Commodity Summaries 2024 estimated global copper mine production at about 22 million metric tons in 2023. That volume helps explain why wear life, crusher availability, and maintenance planning matter. Small details matter. Feed size, moisture, abrasiveness, and particle shape can all influence how a mantle and concaves wear in service.

A practical selection begins with the material being crushed and the crusher’s operating conditions. Review the alloy and heat treatment, but also check part fit, chamber profile, feed distribution, and the wear pattern on removed components. Manganese steel may suit some applications, yet no grade is ideal for every ore or operating setup. Ask suppliers for documented material specifications and comparable application history, then compare expected service life and changeout time—not purchase price alone. The right choice is the one that performs consistently in your conditions. That sounds straightforward. It is not always. Wear records can be incomplete, and one successful trial does not prove a universal result. This guide explains how to assess Gyratory Crusher Wear Parts with evidence, operational context, and a clear view of the trade-offs.
How to Choose Gyratory Crusher Wear Parts?

Identify the Crusher Model and Operating Conditions

How to Choose Gyratory Crusher Wear Parts?

Identify the Crusher Model and Operating Conditions

Start with the crusher’s exact model, serial number, and configuration. Check the equipment plate and current technical drawings; similar-looking machines may use different mantle or concave profiles. Record the chamber type, feed opening, eccentric throw, and installed wear-part dimensions. Small differences matter. A part that fits physically may still produce poor nip or an unsuitable discharge profile.

Then document what the crusher actually processes. Note feed-size distribution, rock type, moisture, abrasiveness, throughput, closed-side setting, and operating hours. The USGS Mineral Commodity Summaries 2024 estimated U.S. crushed-stone production at about 1.5 billion metric tons in 2023. That scale covers very different feed materials and operating duties, so a generic wear recommendation is risky. Keep samples and shift records. Useful clues.

Inspect Wear Patterns

Inspect wear patterns across the mantle and concaves, not just the thinnest spot. Uneven wear can point to feed segregation, bridging, or an off-center feed stream. Compare measured wear with past inspections and the crusher’s service limits. The first estimate is often wrong; field notes can be incomplete. Still, consistent measurements help narrow the correct profile and material specification before ordering.
Compare Wear-Part Materials and Design Options

How to Choose Gyratory Crusher Wear Parts?
Compare Wear-Part Materials and Design Options

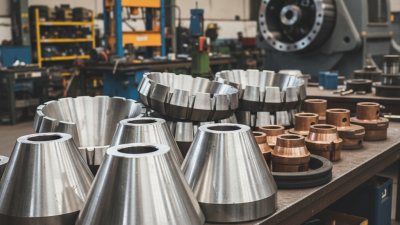
Material choice depends on impact, abrasion, and the rock entering the chamber. Austenitic manganese steel is widely used for mantles and concaves because repeated impact can work-harden its surface. It suits coarse, tough feed. In lower-impact conditions, alternative alloy compositions may resist abrasion differently, but hardness alone is not a reliable selection rule. There is no perfect liner.

The USGS Mineral Commodity Summaries 2024 estimated U.S. crushed-stone production at about 1.5 billion metric tons in 2023. That scale makes unplanned wear costly, but the figure does not predict wear life at a specific site. Match the profile to feed size, chamber geometry, and the required product. A steep profile may help with coarse feed; a different cavity can improve reduction or throughput. Check the crusher’s operating limits before changing geometry.

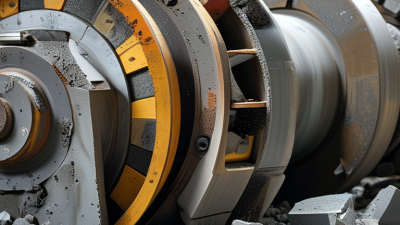
Inspect the removed parts. Polished high spots, deep grooves, and uneven ledges can reveal where contact and wear concentrate. Useful evidence. Compare these patterns with feed records and operating settings before ordering replacements. Thicker sections may last longer, yet they can also restrict capacity or shift wear elsewhere. A small doubt is healthy: operating conditions change, and one successful liner design may not repeat across every rock type.

How to Choose Gyratory Crusher Wear Parts? — Compare Wear-Part Materials and Design Options
Decision factor Option Typical characteristics Best suited to Trade-offs and checks
Wear-part material Austenitic manganese steel, approximately 11–14% Mn Work-hardening steel that can develop a harder surface under impact while retaining a relatively tough core. Applications with substantial impact and compressive loading, where the feed is sufficiently hard to work-harden the surface. May wear rapidly if the feed is too soft to produce adequate work-hardening. Actual composition and performance vary by casting specification and operating conditions.
Wear-part material Higher-manganese steel, commonly around 18% Mn Offers a manganese-steel option for applications where a different balance of work-hardening response and toughness is needed. Some medium- to high-impact crushing duties; selection should be based on feed characteristics and measured wear history. Higher manganese content alone does not guarantee longer life. Confirm suitability with the crusher and wear-part supplier’s application guidance.
Wear-part material High-manganese steel, commonly around 22% Mn Another work-hardening manganese-steel grade; its benefit depends on alloy specification, heat treatment, and the operating environment. Trial applications where operating data indicates that this grade may improve service life or wear distribution. Can increase purchase cost without improving life in every duty. Compare cost per tonne and inspect for cracking or unusual wear.
Wear-part material Alloyed manganese steel Manganese steel with controlled alloy additions intended to modify properties such as strength, toughness, or wear response. Applications where a standard manganese grade has shown a specific, documented limitation. Alloy additions and results are specification-dependent. Request material certificates and compare against service data from the same crushing conditions.
Concave profile Coarse profile Uses a coarser crushing-zone geometry than a fine profile. Primary crushing of larger feed, when the crusher configuration and required product size allow it. Check feed-size distribution, setting, chamber fit, and the potential effect on throughput and product gradation.
Concave profile Fine profile Provides a different chamber geometry intended for a smaller feed range or a more advanced crushing duty. Applications with appropriately sized feed and a product-size target compatible with the crusher’s design. May be unsuitable for oversized or poorly controlled feed. Confirm the recommended feed range and compatibility with the installed mantle.
Mantle and concave pairing Matched chamber set Mantle and concaves are selected together to maintain the intended crushing profile and wear pattern. Routine replacements and profile changes where the crusher manufacturer’s configuration guidance is available. A mismatched combination can alter chamber geometry and performance. Verify part compatibility, installation sequence, and allowable settings.
Profile-life strategy Standard profile Uses a conventional chamber profile for the specified crusher and application. Stable operations with known feed properties and established wear-part performance. Use wear measurements and operating records to confirm that the profile makes effective use of the available wear material.
Profile-life strategy Application-optimized profile Profile geometry is selected or adjusted to address a measured issue such as uneven wear or poor chamber utilization. Operations with reliable data on feed size, throughput, power draw, settings, and liner wear. Changes should be checked for crusher compatibility and evaluated through controlled trials; a modified profile is not automatically an improvement.
Selection and validation Operating-condition review Considers feed hardness and abrasiveness, particle-size distribution, moisture, throughput, crusher setting, and operating practices. Every material or profile selection, especially when changing from an established liner specification. Track tonnes processed, service hours, wear distribution, downtime, and cost per tonne. Results from one site may not transfer directly to another.
Material grades and profile names are not fully standardized across suppliers. Confirm the crusher model, compatible part dimensions, material specification, and application recommendations before ordering or changing a wear-part design.

Match Components to Feed Characteristics and Crushing Stage

Match the mantle and concaves to what actually enters the crusher, not just the rock name. Record feed-size distribution, moisture, clay content, and silica level across several shifts. Coarse, blocky feed can concentrate impact near the chamber entrance; highly abrasive feed can wear contact surfaces faster. ASTM C131/C535 abrasion-test results report aggregate mass loss as a percentage, offering a useful screening measure. It is not a direct prediction of liner life. Not a perfect forecast.

The crushing stage matters too. A primary gyratory handling large, uneven run-of-mine feed needs a profile that accepts those lumps without choking. At later stages, tighter settings and finer feed may shift wear toward other chamber zones. Compare mantle and concave wear maps after inspections, then adjust component profile or material to match the observed pattern. The SME Mineral Processing and Extractive Metallurgy Handbook discusses feed properties and crushing conditions as key process variables; use those measurements alongside site records, not as substitutes for them. One practical detail: wet fines can pack between larger stones, so a dry-feed assumption may mislead. Review the chamber after a representative production run, because one short inspection can capture an unusual feed day.

How to Choose Gyratory Crusher Wear Parts? — Match Components to Feed Characteristics and Crushing Stage

Use the feed condition to guide liner selection: coarse feed with high impact calls for toughness, while hard, abrasive feed increases the importance of abrasion resistance. Manganese steel can work-harden under impact. These 1–5 scores are qualitative selection priorities, not measured wear rates or guarantees; confirm mantle and concave profiles against the crusher stage, feed size, and closed-side setting.

Check Fit, Compatibility, and Installation Requirements

Before selecting gyratory crusher wear parts, confirm the exact crusher model, serial range, and chamber configuration. A mantle or concave can look correct yet differ in profile, seating dimensions, or required clearances. Small mismatches matter. Compare part drawings and key measurements with the machine’s approved documentation, rather than relying on appearance alone. Check that the wear profile suits the feed size and operating setup; a poor match may cause uneven contact or faster wear. If records are incomplete, measure the removed part and verify details with a qualified service technician.

Review installation requirements before the parts arrive. Confirm lifting points, handling equipment, fastening hardware, and the specified tightening procedure. Clean and inspect contact surfaces, then check that the component seats evenly without debris or visible gaps. Do not force it. Forcing a part can damage seating surfaces or hide an alignment problem. Follow the equipment manual for assembly sequence and clearances, since procedures vary by design. After installation, rotate or inspect the assembly as directed, and recheck fasteners and clearances at the recommended interval. I would still question any fit that depends on excessive adjustment; it may signal an incompatible part or an overlooked measurement.

Track Wear Patterns and Adjust Replacement Choices

How to Choose Gyratory Crusher Wear Parts?

Track Wear Patterns and Adjust Replacement Choices

Wear patterns reveal how a gyratory crusher is working, not just how long its parts have been installed. During inspections, compare the mantle and concave surfaces at several points around the chamber. Uneven wear near the feed opening may point to poor feed distribution or a changing rock mix.

A polished band, deep grooves, or local cracking each tells a different story. Take photos from consistent angles and record operating hours, feed size, and material conditions. Small details matter.

Replacement choices should reflect those observations. If wear is concentrated in one zone, review feed flow and chamber fit before selecting a different profile. A harder alloy may last longer in some applications, but it can also respond poorly to impact or abrasive conditions. Check the crusher maker’s technical guidance and consult a qualified service specialist when damage is unusual.

Measure remaining thickness; visual estimates can mislead. They often do. Keep records across several changeouts, since one inspection rarely proves a trend. And be honest about gaps in the data. A rushed note from a dusty shutdown may not support a confident decision. When wear becomes uneven sooner than expected, investigate the operating conditions before simply ordering the same parts again.